Small Scale Gasification Plant: Sizing It to Your Feedstock
Most people searching for a small scale gasification plant already know what gasification is. What they do not have is the arithmetic: how many tonnes a year make how many kilowatts, how much heat and char come out, how many hours a year the plant can be counted on, and what the feed has to look like before any of it works.
The search results do not give it to them. They split into academic reviews on one side and vendor spec tables on the other. Yet the measured data exists. A monitoring campaign on the commercial small-scale plants in South Tyrol, Italy, published full mass and energy balances for eight technologies. This guide turns those ratios into a five-step sizing method, then shows the catch every one of them hides.
We build in this class ourselves. The X-150 is a 150 kg/h fixed-bed downdraft gasifier, so we will use it where it helps and say plainly where the published ratios do not apply to it.
What counts as a small scale gasification plant
There is no single definition. A 2021 technical review found upper limits from 100 kW to 500 kW of electrical output in the literature, settled on below 500 kWe because that is roughly the ceiling of the fixed-bed reactor, and noted that small plants still convert biomass to electricity at above 20% on average (Allesina and Pedrazzi, MDPI Energies).
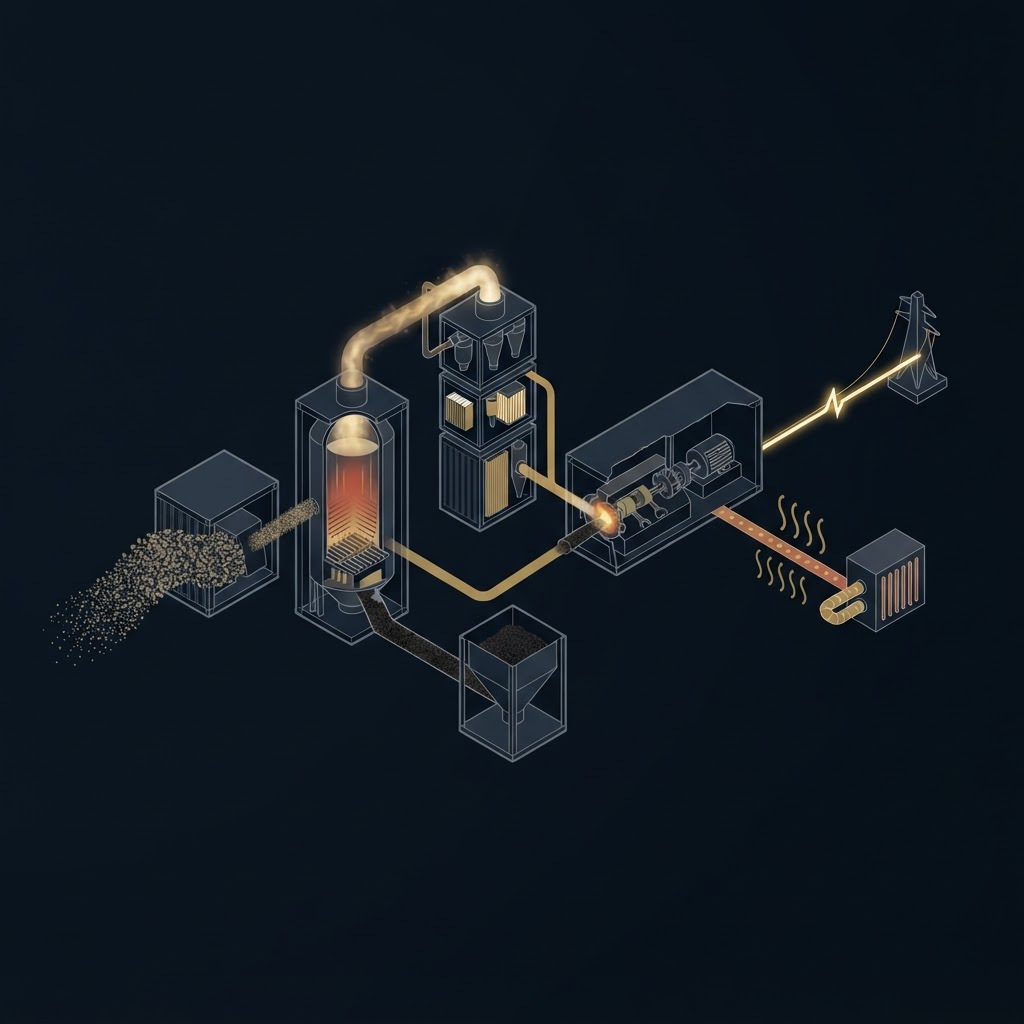
Whatever the size, the plant has the same five blocks: feed preparation, the reactor, gas cooling and cleaning, a gas engine with a generator, and char and ash handling. Almost all of them use an internal combustion engine, because engines are cheap to repair and spare parts are everywhere. That choice forces the gas to be cooled and cleaned of tar, which is where most of the engineering goes.
If you are weighing a single containerized unit rather than a plant with several blocks on a site, start with containerized waste to energy, which covers what fits in the box and what does not.
Sizing a plant in five steps
Step 1: tonnes per year to kg/h
Size on dry tonnes, not wet ones, and on hours the plant will actually run.
The South Tyrol campaign found that manufacturers of commercial plants below 200 kWe guarantee 7,000 hours a year, with 8,000 being the norm (South Tyrol monitoring review, Energy). So the divisor is 7,000 to 8,000, not 8,760.
The formula is simple: dry kg per year divided by run hours gives the design feed rate in kg/h.
Step 2: kg/h to electricity and heat
The representative measured figure for well-run commercial plants is 1.10 kWh of electricity per kg of dry biomass, from the same campaign. Its other averages are the ones to plan with:
| Measured parameter (South Tyrol, 8 technologies) | Average |
|---|---|
| Cold gas efficiency (energy in gas vs energy in biomass) | 74.3% |
| Net electrical efficiency | 19.9% |
| Thermal efficiency | 48.3% |
| Total CHP efficiency | 68.3% |
| Plant self-consumption of electricity | 12.7% |
| Dry biomass per kWh, by technology | 0.71 to 1.05 kg |
Two things follow. First, a small gasification plant is a heat plant that also makes power: it delivers about 2.4 kWh of heat for every kWh of electricity. Without a heat customer you are throwing away more than half the output. Second, self-consumption ranged from 8.1% to 23.8% of gross generation, so always ask whether a quoted kWe is gross or net.
Rated and pilot figures are less generous than the best monitored plants, and the spread is worth knowing before you read a quote:
- RESET's SyngaSmart rates 60 kg/h of biomass for 50 kWe, about 1.2 kg per kWh (RESET).
- FAO's worked example for a producer gas engine lands at 1.35 kg per kWh, at 14% moisture and 70% gasifier efficiency (FAO).
- An All Power Labs unit tested for the California Energy Commission improved from 1.2 to 1.0 kg per kWh over more than 750 hours (California Energy Commission).
- Loopura's ladder rates 50 kg/h of dry chips for 30 kW gross, about 1.7 kg per kWh (Loopura).
- A Brazilian pilot downdraft plant needed 1.9 kg per kWh at 17% electrical efficiency (Chaves et al.).
For a first sizing, plan on 1 to 1.5 kg of dry feed per kWh of electricity. Anything better than 1 kg needs measured proof.
Step 3: what you get besides power
Char. The plants in South Tyrol are tuned to maximise gas, so char stays below 5% of the feed and typically at 1 to 2%. Designs that value biochar make far more: RESET's 50 kWe module gives 4.2 kg/h of biochar from 60 kg/h, about 7%, and Loopura's design basis is 35 tonnes of biochar from 350 tonnes of feed, 10%. Every kilogram of carbon left in the char is energy that did not reach the engine, so decide early whether you are building a power plant or a biochar plant that also makes power.
Gas quality. Air-blown gasification dilutes the gas with nitrogen. The South Tyrol plants averaged 47.1% nitrogen and 18.1% hydrogen in dry gas, at a heating value of 4.96 MJ/kg. That is fine for an engine and useless for hydrogen. Our X-150 runs an oxy-steam mode that removes the nitrogen ballast: in the COMETHA campaign the syngas held 33% hydrogen at an H2 to CO ratio of 1.95 to 1 (Zero-X on LinkedIn). If hydrogen or chemicals are a future revenue line, the gasifying agent is a sizing decision, not a detail. The planned guide to oxy-steam gasification goes deeper.
Step 4: the hours you can count on
The 7,000 to 8,000 hours above are manufacturer guarantees on selected wood, and they assume someone on site every day. Small gasifiers need daily maintenance operations, against monthly or yearly visits for solar and wind, and most existing designs cannot run below nominal power, so they do not follow a load (Allesina and Pedrazzi). Size the plant to run flat out on a steady base load and let the grid or a battery take the peaks.
Step 5: what the feed has to look like at the reactor
This step decides whether steps 1 to 4 hold at all. Commercial fuel specs are strict:
| Maker | Moisture limit | Other requirement |
|---|---|---|
| Spanner | below 13% | under 30% fines below 4 mm |
| Holz Energie | below 10% | chips 50 to 70 mm, no fines |
| RESET | 12% | chipped residues, nut shells, briquettes |
| Glock | 30% | P16 to P31 chips, 15% bark and fines allowed |
| Powermax TFBG | 20% | 20 to 80 mm |
Sources: Allesina and Pedrazzi, Powermax.
Drying changes the mass you size on. 1,000 kg of residue at 50% moisture holds 500 kg of dry matter; dried to 15% it weighs about 590 kg. The dryer, the chipper or pelletizer and the covered store are part of the plant, and the obvious energy source for the dryer is the plant's own heat. That is one more reason the heat line in step 2 matters. More on that in the planned guide to gasifier feedstock moisture content.
A worked example: 1,000 tonnes a year of dry wood residue
An illustration with the ratios above, not a quote.
- Feed rate: 1,000,000 kg over 7,500 hours is about 133 kg/h.
- Electricity: at 1 to 1.5 kg per kWh, roughly 90 to 135 kWe. At the South Tyrol representative 1.10 kWh per kg, about 145 kWe.
- Heat: about 2.4 times the electrical output, so roughly 220 to 350 kWth to place.
- Char: 10 to 20 tonnes a year if tuned for power, 70 to 100 tonnes if tuned for biochar.
- Format: one or two vendor modules in the 50 to 200 kWe range, or one X-150 running at 150 kg/h with headroom.
The same arithmetic for one X-150 at its rated 150 kg/h over 7,500 hours is about 1,125 tonnes of feed a year, roughly 3 tonnes a day. We do not publish a kWe figure for it on waste, because electricity per kg depends on the heating value of the waste, and that is exactly the variable the next section is about.
The catch: every ratio above was measured on wood
Look back at the fuel table. Every commercial small-scale design on it runs on wood chips or pellets, and the measured ratios come from plants burning them. The South Tyrol authors say it directly: high-quality feedstock is currently a prerequisite, and agricultural waste still presents several challenges.
The reason is history. Many of these designs were developed under feed-in tariffs. Italy paid 229 EUR/MWh for small biomass power from 2012 to 2016, which rewarded complex plants running on selected, expensive fuel. The result is a market of good machines for clean wood: Spanner has over 700 grid-connected plants and Burkhardt about 200 on EN plus A1 pellets, while most single-throat downdraft reactors need low moisture and low ash to avoid slagging (Allesina and Pedrazzi).
Put waste through that machine and the gas goes off spec. Thomas Reed, one of the fathers of fixed-bed gasification, summed up the usual project: a new gasifier is built, the gas turns out to contain 0.1 to 10% tar, and the rest of the time and money is spent on that problem. If your feedstock is sludge, municipal waste, digestate, straw or husks, tar removal from syngas is the section of the design to read first.
This is the gap the X-150 is built for. It has been validated at Paris COMETHA, at Verkoso with Fraunhofer IKTS and at Hochschule Zittau/Goerlitz on high-ash sewage sludge, municipal waste and digestate, the feedstocks that clean-wood gasifiers clinker on (Zero-X). Its longest public run is 1,939 continuous hours in Paris, 80 days, processing 16,382 kg of digestate pellets at 99.98% tar conversion. When you size a plant on waste, that kind of number, continuous hours on a named difficult feedstock, is the one to demand from any vendor, ours included.
One big unit or several small ones
Small plants are already built from multiples. RESET puts up to four gasification units on one skid. Powermax serves 600 kW with two gensets and 1,200 kW with three. Loopura's 500 kW plant takes four 40 ft container equivalents against one for its 30 kW mobile unit.
Multiples make sense for three reasons:
- Turndown. A plant that cannot run below nominal follows a falling feed supply by switching units off, not by throttling.
- Availability. One unit in maintenance leaves the rest running, which matters when daily maintenance is the norm.
- Growth. Feed supply rarely arrives at full volume on day one.
For a site with 3 tonnes a day, one 150 kg/h reactor fits. At 10 tonnes a day, about 420 kg/h, three units with shared feed preparation and storage are worth comparing against one bespoke reactor. Far above that you leave the small class altogether; the larger plant classes are covered in waste to energy gasification plant.
What the plant costs to carry
The review is blunt: CAPEX and OPEX of small gasification power plants are often too high to sustain the investment without high subsidies for electricity. That is why sizing matters so much. An oversized plant pays for kilowatts it never has the feed to make.
Two levers change the picture. Revenue from what you stop paying for, such as waste hauling and diesel, can matter more than the value of the power. And public capital: in our target markets governments fund 56 to 70% of project CAPEX. The detailed numbers are in what it costs to build a waste to energy plant and, by country, in government grants for waste to energy.
Questions that size the plant before a vendor does
- How many dry tonnes a year do you control under contract? Measured, not estimated, and at what moisture.
- What is the ash content of the feed? High ash is what stops wood-rated reactors.
- Who buys the heat? Heat is more than half the output.
- Which product is the plant for: power, heat, hydrogen or biochar? Each moves the design.
- What continuous hours has the vendor logged on your feedstock, not wood?
- Is the quoted kWe gross or net of self-consumption?
- Who does the daily maintenance, and are they trained and on site?
Size the plant to the waste you control, and make the vendor prove the ratios on that waste.
FAQ
How much biomass does a small gasification plant need per kWh? Monitored commercial plants in South Tyrol use 0.71 to 1.05 kg of dry wood per kWh of electricity. Rated and pilot figures run from about 1.2 to 1.9 kg per kWh, so 1 to 1.5 kg is a safe planning range.
How many hours a year can a small scale gasification plant run? Manufacturers of small commercial plants guarantee 7,000 hours a year and 8,000 is the norm, on selected wood with daily maintenance. On waste, ask for continuous hours on your own feedstock.
Can a small scale gasification plant run on waste instead of wood? Most commercial designs cannot; they require dry, low-ash wood chips or pellets. Waste-rated designs exist, but they need validation on the specific waste, such as the X-150's runs on sludge, municipal waste and digestate.
How much space does a small scale gasification plant need? Less than people expect for the reactor: a 50 kWe skid can be 3.5 by 2.4 m, and a 500 kW plant around four 40 ft container footprints. Add room for feed storage, drying and the heat connection on top.
We use cookies to improve your experience on this site. By continuing, you agree to our Privacy Notice.